Describe the problem in your own words. AI picks the services, solutions and articles on our site that fit it.

    Manufacturing

    A shop floor that reports what is happening on it

    Machine states, piece counters and downtime enter the system straight from the controllers. The operator confirms the operation on a screen at the machine, and the planner and accounting see the same thing right away.

    Does this sound like your shop floor?

    OEE calculated in the morning from paper

    The operator writes pieces and downtime on a job card, someone types them into a spreadsheet the next morning. You know the shift's result a day later, when nobody remembers why the machine stopped.

    Work in progress visible only from the floor

    The salesperson calls the shift manager to tell a customer which stage their order is at. The manager walks over to check.

    A batch with no trail when a complaint comes in

    The batch number is on the label, but the raw material, machine and operator mean searching the QC binder and job cards. The answer to the customer takes days.

    Eight parts that make up the system

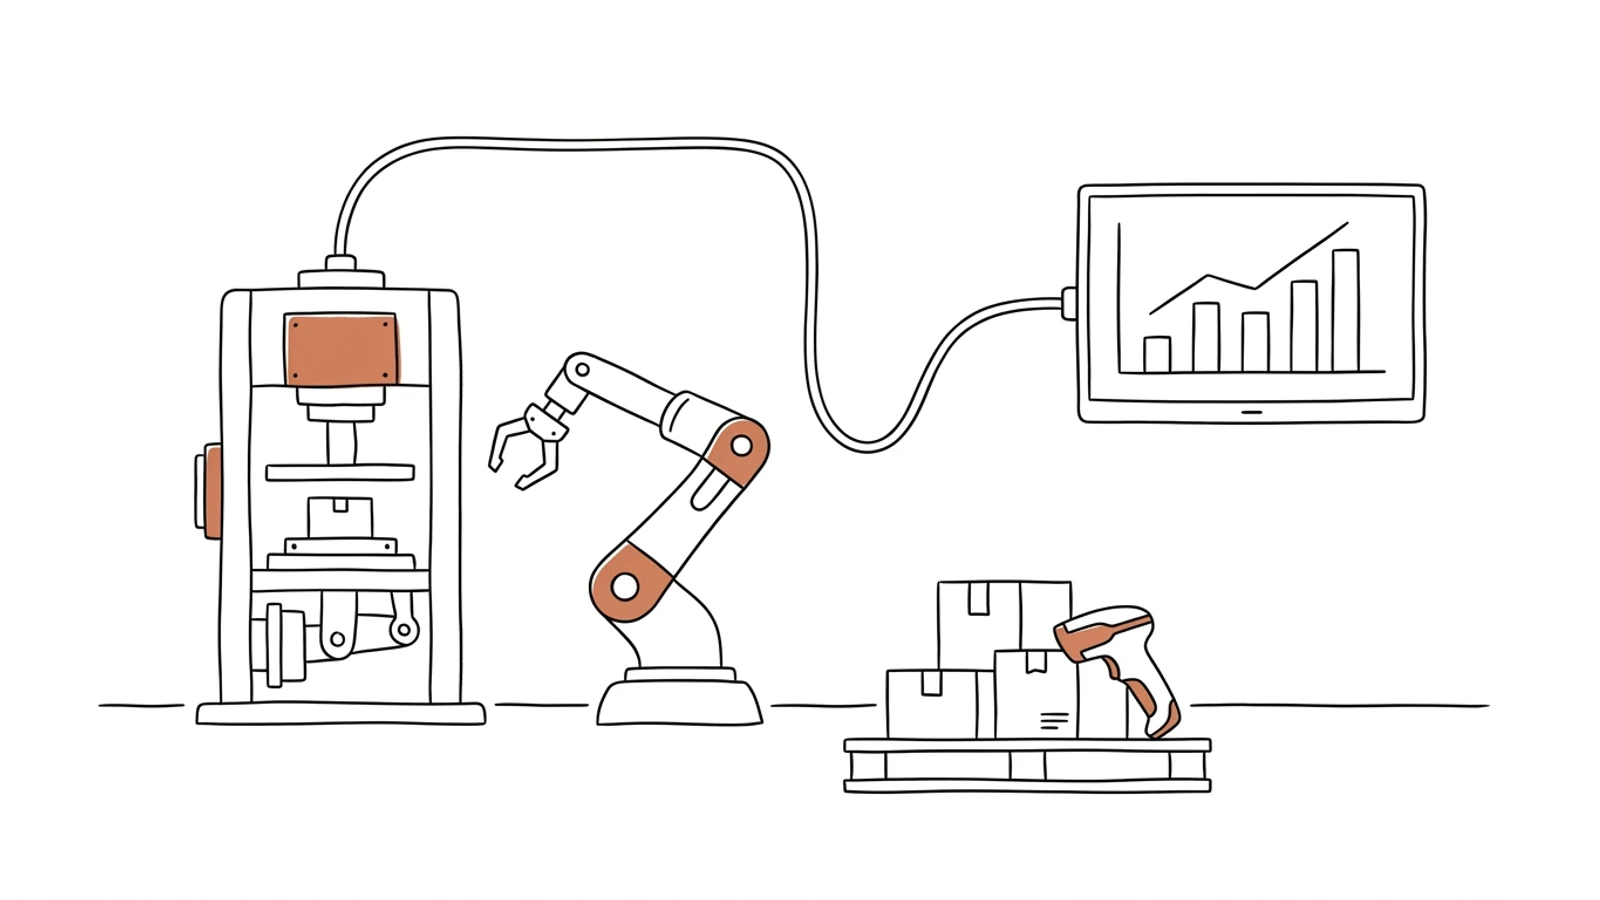
    The scope depends on the machines: one setup for CNC work centers, another for a food line with batches. Controllers and SCADA stay.

    Machine connectivity

    States, counters and alarms from Siemens, Beckhoff and other controllers over OPC UA, Modbus or from SCADA. Older machines get a sensor and a counter.

    Operator panel at the machine

    The order, drawing and process sheet on a screen at the workstation. The operator starts the operation, reports downtime with a reason and confirms pieces with one tap.

    Live OEE per work center

    Availability, performance and quality calculated from machine data and operator reports. The manager sees during the shift which work center is down and why.

    Work-in-progress tracking

    Every order has a stage, a work center and a piece count. The salesperson answers the customer from the system, without calling the floor.

    Batches and product genealogy

    Raw material, semi-finished part, machine, operator and QC result linked to the batch number. A label scan from a Zebra handheld closes the chain.

    Quality control from the floor

    Inspection plans, measurements typed in or read from gauges, non-conformances with a photo. The QC record is created at the machine.

    Data exchange with ERP and planning

    The order comes down from the ERP to the floor, completion and consumption go back to the ERP and the plan.

    Alerts

    Downtime longer than usual, a drop in pace, no reason reported. The notification goes to the shift manager.

    What AI does in the MES

    Three years ago features like these needed a data science team. Today language models read emails, documents and photos, and we build them into the system we make for you. Below is what makes sense in this solution. A person approves, AI prepares.

    Downtime predicted from history

    The model learns from downtime history, alarms and machine parameters. When a pattern resembles previous failures, it warns maintenance before the machine stops.

    Example a rising number of micro-stops on the press over the last three shifts → a maintenance ticket with a list of similar cases
    Job cards and QC reports read

    A photo of a handwritten job card or measurement report becomes data to confirm. Useful at machines with no screen.

    Example a job card photo with "feeder jam 20 min" written on it → downtime with a reason on the order, ready to approve

    Ask the shop floor

    The manager asks in plain language, the answer comes from machine and order data.

    Example "why did work center 4 make less than planned yesterday?" → three downtime events with reasons and durations

    Scrap causes grouped

    AI groups the week's QC non-conformances by machine, operator, raw material batch and shift. The process engineer decides.

    Example 12 dimensional non-conformances in a week → all from one batch of bar stock, a proposed supplier complaint

    Effects you see in the first month

    • OEE is visible during the shift, because it is calculated from the machine counters
    • The salesperson tells the customer the order stage from the system, without a call to the floor
    • A batch complaint has its full genealogy in a minute: raw material, machine, operator, QC result
    • Material consumption and machine time return to the ERP after every operation, so order cost is current
    What it connects to

    Works with your machines and systems

    We do not replace controllers or rebuild SCADA. We read what the machines already send and hand the data to the ERP and planning.

    Siemens S7Beckhoff TwinCATOPC UAModbus TCPMQTTSCADAZebraHoneywellComarch ERP XLenova365SAP Business OneStreamsoft PrestiżImpuls EVOmeasuring instruments

    Work center by work center

    We start with the few machines that hurt most. The rest of the floor joins once the first work center is running.

    01

    Machine and process analysis

    We walk the floor with the production manager and maintenance. We write down machines, controllers, interfaces and everything recorded by hand today.
    2–3 weeks
    02

    Pilot on one work center

    A few machines connected, operator panel, OEE and order tracking for one work center. Data exchange with the ERP from day one.
    8–10 weeks
    03

    Further work centers, batches and QC

    More machines, batch genealogy, quality control at the workstation, alerts to managers.
    3–4 weeks each
    04

    Maintenance and development

    New machines, new reports, downtime prediction models. You set the queue.
    ongoing

    Does your company run on Excel, emails and a system from years ago? We will build the solution that puts it in order, with AI inside from the start.

    You have the diagnosis, we build the solution. Web applications, B2B portals and automations for companies without a large IT department. Today a system can read emails and documents, suggest decisions and answer customers on its own, so we build that in from the first version, not as an add-on a year later.

    We agree scope, price and dates upfront, show progress every week, and the code and data stay yours.

    • scope, price and dates upfront
    • progress every week
    • your code and data

    Common questions

    Do we have to replace controllers or SCADA?
    No. We read controller data over OPC UA or Modbus, and if SCADA already collects it, we take it from there. Machines without an interface get a counter or sensor.
    What about machines from the nineties?
    We fit a rotation sensor, a piece counter or a current measurement, and the operator confirms the rest on screen. That is enough for OEE and order tracking.
    Will the operators use it?
    The panel starts with three buttons: start, stop, downtime. Training takes 20 minutes at the machine.
    Does it work without Wi-Fi on the floor?
    Controllers are usually on a wired network and that is where the data travels. Panels and handhelds work offline and send data when coverage returns.
    Who owns the code and the data?
    You do. Machine data sits in your database, the code in your repository. You can change vendors at any point.

    Updated:

    Let's talk about your shop floor

    You tell us which machines you run and what goes on job cards today, we tell you which work center to start with.

    Write to us
    or email hello@udb.plhello@udb.pl